A DT4C Iron Core for Latching Relay must generate sufficient magnetic force with a short excitation pulse while maintaining a controlled magnetic state after coil power is removed. DT4C and DT4E electric pure iron are used for magnetic relay components because their low carbon content, high magnetic permeability, and controllable coercivity can support efficient magnetic circuits when the material condition, forming process, and annealing cycle are properly controlled.
For smart-meter and low-power switching applications, the engineering target is not simply "high magnetism." The core must maintain repeatable magnetic response, dimensional stability, low residual stress, and controlled surface protection across production batches.
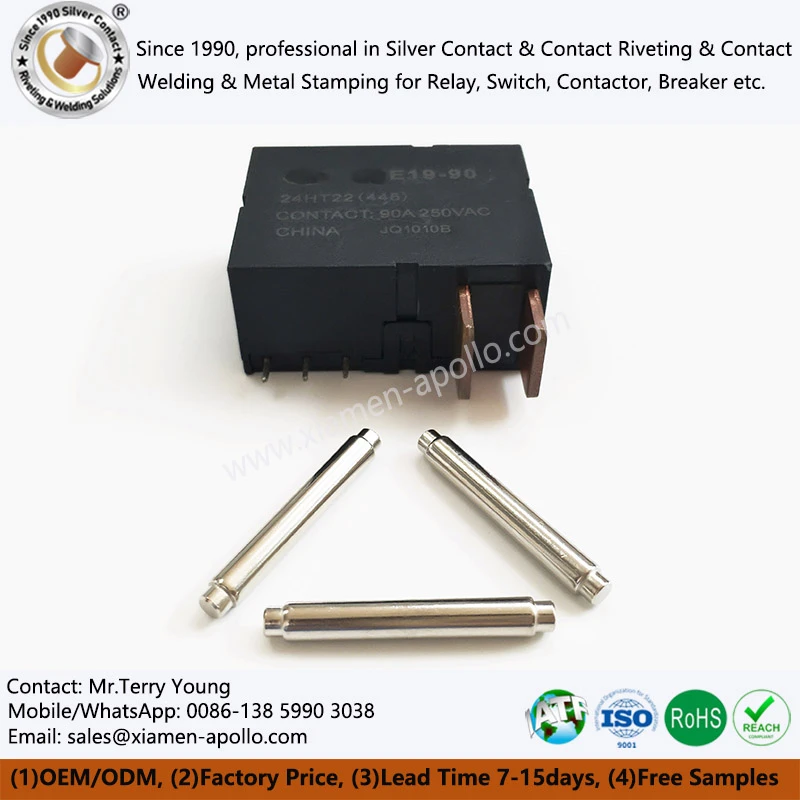
DT4C / DT4E Material Control for Electromagnetic Iron Cores
Electrical pure iron grades such as DT4C and DT4E are selected for magnetic components where magnetic properties are more important than mechanical strength.
Typical production control should cover:
- Chemical composition according to the specified DT4 grade
- Low carbon and impurity content
- Initial material thickness and dimensional tolerance
- Magnetic permeability and coercive-force requirements
- Microstructure after forming and annealing
- Surface condition after stamping, machining, or grinding
- Lot-level material traceability
| Engineering factor | DT4C / DT4E control point | Effect on relay core |
|---|---|---|
| Carbon and impurities | Controlled according to material specification | Influences magnetic losses and permeability |
| Magnetic permeability | Verified against drawing or technical specification | Determines magnetic flux response |
| Coercive force | Controlled after annealing | Affects magnetic hysteresis and release behavior |
| Hardness | Checked after forming/annealing | Indicates process condition |
| Dimensional tolerance | Controlled from drawing | Directly affects air gap and magnetic force |
| Surface condition | No burrs, cracks, heavy scale, or contamination | Protects assembly and coating quality |
| Traceability | Heat/lot identification | Supports IATF 16949 process records |
Smart Meter Latching Relay Cores and Low-Power Coil Operation
A latching relay differs from a conventional continuously energized relay because the coil normally receives a short electrical pulse to change state rather than remaining energized throughout the operating period.
The magnetic circuit therefore has to convert a limited electrical pulse into sufficient mechanical movement.
The practical relationship can be simplified as:
Coil electrical energy → magnetic field → core flux → armature force → contact switching
Small changes in the iron core can influence this chain. For example, excessive residual stress from stamping may alter magnetic permeability. A burr at the pole surface can modify the effective air gap. Poor dimensional control can change the armature/core alignment.
For smart-meter relays, these effects can become relevant because the switching mechanism may be required to operate repeatedly while the overall meter architecture limits available coil energy.

DT4C / DT4E Stamping Stress and Magnetic Performance Control
Progressive die stamping is efficient for high-volume relay-core production, but plastic deformation introduces residual stress into the material. The affected zone is particularly important around punched edges, bends, holes, and pole faces.
Punching Burrs, Residual Stress and Air-Gap Control
The magnetic circuit is highly sensitive to the effective air gap.
A simplified magnetic-reluctance relationship is:
ℜ ≈ l / (μA)
where:
- ℜ = magnetic reluctance
- l = magnetic path length
- μ = material permeability
- A = effective magnetic cross-sectional area
The equation shows why a small dimensional deviation at the pole interface can influence the magnetic circuit even when the bulk material remains unchanged.
For precision relay cores, process control should therefore include:
- Punch clearance verification
- Burr-height monitoring
- Pole-face flatness
- Hole-to-reference dimensional control
- Bend-angle control where applicable
- Progressive-die wear monitoring
- Lot-based dimensional inspection
A practical production drawing may specify dimensional tolerances such as ±0.03 mm, ±0.02 mm, or tighter values depending on the magnetic circuit and assembly structure. The tolerance should be established from the actual relay design rather than applied as a generic value.
Why Annealing Is Required After Cold Working
Cold heading, stamping, bending, and machining can increase dislocation density and residual stress.
For a magnetic core, this is not only a mechanical issue. Internal stress can change magnetic-domain movement and increase the magnetic field required for domain-wall motion.
Vacuum annealing is therefore used to restore a more stable microstructure and reduce the magnetic impact of forming stress.
| Process condition | Magnetic effect | Production concern |
|---|---|---|
| As‑stamped pure iron | Higher residual stress | Magnetic properties may vary |
| Stress‑relieved material | Reduced internal stress | More stable magnetic response |
| Proper vacuum annealing | Improved domain mobility | Lower coercive force may be achieved |
| Excessive thermal exposure | Grain growth / dimensional change risk | Requires cycle validation |
| Inadequate annealing | Residual stress remains | Magnetic consistency may suffer |
Vacuum Annealing Parameters for Relay Core Production
Annealing must be validated against the actual DT4C/DT4E material thickness, geometry, furnace atmosphere, loading condition, and target magnetic properties.
The production specification should normally define:
- Heating rate
- Annealing temperature range
- Holding time
- Vacuum or controlled-atmosphere condition
- Furnace loading
- Cooling rate
- Post-annealing surface condition
- Magnetic-property verification
Rather than assigning one universal temperature or holding time to every relay core, the process window should be established through material trials and magnetic-property testing.
The key objective is to reduce residual stress without creating unacceptable dimensional change, surface oxidation, grain-structure variation, or distortion.
Consult Our Electrical Engineers Today
Coercive Force, Permeability and Hysteresis Control in Latching Relay Iron Cores
The magnetic performance of a relay core should be evaluated through measurable parameters rather than visual inspection alone.
Coercive Force and Residual Magnetism
Coercive force indicates the reverse magnetic field required to reduce magnetization toward zero after magnetization.
For a latching relay, the magnetic circuit must be designed around the required operating and release conditions. Excessive residual magnetism can affect release behavior in some magnetic structures, while insufficient magnetic force can prevent reliable state transition.
The correct target therefore depends on:
- Coil ampere-turns
- Core geometry
- Pole-face area
- Air gap
- Permanent magnet configuration
- Armature mass
- Spring force
- Required switching time
- Operating temperature
A core supplier should not specify coercive force independently from the relay's magnetic-circuit design.
Magnetic Testing for Production Lots
A production QA plan can combine material certification, dimensional inspection, hardness testing, and magnetic testing.
| Test item | Typical engineering purpose | Recommended control basis |
|---|---|---|
| Chemical composition | Confirm material grade | Material certificate / specified DT4 grade |
| Dimensional inspection | Confirm magnetic geometry | Customer drawing |
| Burr inspection | Control pole and assembly interface | Customer drawing/process standard |
| Hardness / micro‑hardness | Verify thermal and forming conditions | Approved process specification |
| Coercive force | Evaluate magnetic hysteresis | Agreed magnetic test method |
| Permeability / B‑H characteristics | Verify magnetic response | Agreed test method |
| Surface inspection | Detect oxidation or defects | Visual/microscopic inspection |
| Plating thickness | Verify corrosion‑protection layer | Coating specification |
| Lot traceability | Link product to raw material and process | IATF 16949 control plan |
For production approval, the magnetic test method must remain consistent between material qualification, process validation, and batch inspection. Changing specimen geometry, demagnetization conditions, or test equipment can make apparently different results difficult to compare.
Zinc vs Nickel Plating: Corrosion Protection and Magnetic-Circuit Dimensions
Pure iron is susceptible to atmospheric oxidation. A protective coating can therefore be required when the relay is exposed to humidity, condensation, storage conditions, or corrosive environments.
Zinc and nickel are common coating choices, but plating is not simply a corrosion-resistance decision. Coating thickness, surface roughness, dimensional buildup, adhesion, and post-treatment can all affect assembly.
Zinc Plating for Relay Iron Cores
Zinc plating is commonly used where corrosion protection and cost control are important.
Engineering controls can include:
- Zinc coating thickness
- Chromate/passivation system
- Surface coverage
- Adhesion
- Salt-spray resistance according to the specified test requirement
- Hydrogen-related process controls where applicable
- Dimensional buildup at critical magnetic interfaces
ASTM B117 may be specified for salt-spray testing when required by the customer qualification plan, but the exposure duration and acceptance criteria should be defined separately.
Nickel Plating for Magnetic Relay Components
Nickel plating can provide a different combination of surface hardness, wear resistance, corrosion resistance, and appearance.
However, nickel coating should be evaluated together with:
- Plating thickness
- Magnetic permeability of the complete coated structure
- Pole-face dimensions
- Contact/interface requirements
- Coating adhesion
- Corrosion qualification
For precision magnetic circuits, coating thickness should be controlled rather than treated as an aesthetic specification.
Coating and Magnetic-Loss Trade-Off
At the operating frequencies of typical latching relay switching events, coating-related magnetic losses are usually not evaluated in the same way as high-frequency transformer-core losses. The more immediate engineering concerns are dimensional buildup, magnetic-interface geometry, surface condition, and long-term corrosion.
Where the relay architecture includes rapid repetitive switching, the complete magnetic circuit should still be validated under the actual operating waveform and temperature range.
| Factor | Zinc coating | Nickel coating |
|---|---|---|
| Corrosion protection | Strongly dependent on system and thickness | Strongly dependent on system and thickness |
| Surface hardness | Generally lower than nickel | Generally higher |
| Dimensional buildup | Must be controlled | Must be controlled |
| Magnetic‑interface effect | Usually related to geometry/coating thickness | Requires geometry and material evaluation |
| Cost | Often lower | Often higher |
| Application decision | Based on corrosion and cost requirements | Based on corrosion, wear, and surface requirements |
FAQ: DT4C / DT4E Latching Relay Iron Core Procurement
What is the primary advantage of using DT4E over standard carbon steel in latching relay cores?
DT4E features extremely low carbon content (less than or equal to 0.002%) and minimal impurity levels, yielding significantly higher magnetic permeability, lower coercive force (less than or equal to 24 A/m), and minimal residual magnetism compared to standard carbon structural steels.
How does vacuum magnetic annealing affect the mechanical hardness of stamped iron parts?
Vacuum magnetic annealing at 850°C–900°C relieves residual mechanical stresses induced by progressive stamping and promotes grain growth, reducing the micro‑hardness of the iron core to HV 90–110 while optimizing magnetic flux transmission.
What is the standard sample lead time and quality traceability for custom relay iron core development?
Prototype samples with full dimensional inspection reports and material test certificates are delivered within 10 to 15 business days, supported by full IATF 16949 lot traceability.
contact us
For immediate sourcing of DT4C Iron Core for Latching Relay, send the drawing, material grade, magnetic requirements, and annual volume for engineering review, sample planning, and production quotation.